Certified Contact Lens Manufacturing Portfolio
Explore our top-tier OEM, ODM, and wholesale colored contact lens SKUs engineered for high oxygen permeability and visual appeal.
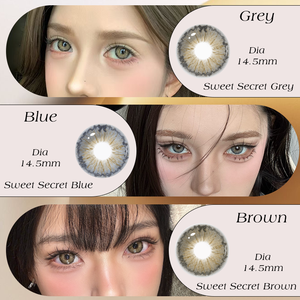
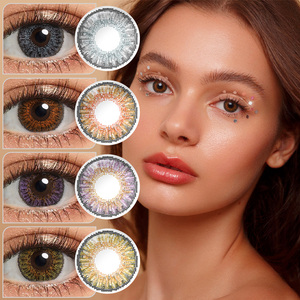
How to Start a Colored Contact Lens Brand: The Complete OEM/ODM Blueprint
A rigorous guide covering optical physics, regulatory compliance, material science, and supply chain management for global cosmetics direct-to-consumer and retail brands.
The global cosmetic contact lens market has evolved from a niche optometric product into a high-growth sector at the intersection of medical devices, optical technology, and personal beauty. Launching a successful colored contact lens brand requires navigating complex regulatory landscapes, selecting appropriate polymer materials, mastering color encapsulation technology, and establishing a resilient, compliant supply chain.
Key Takeaway for Executive Procurement: Colored contact lenses are regulated as Class IIa medical devices in Europe (under CE MDR) and Class II medical devices by the US FDA. Partnering with a fully certified manufacturer holding an FDA Establishment Identifier (FEI) and ISO 13485 quality systems is mandatory to protect brand equity and avoid regulatory impoundment.
Phase 1: Market Intelligence, Audience Mining & Brand Positioning
To establish market share against established optical giants, new brand entrants must execute precise semantic search intent mining and consumer segment targeting. Broad cosmetic claims are no longer sufficient; successful brands specialize in defined product verticals:
- Natural Iris Enhancers (1-Tone to 3-Tone Patterns): Targeting daily wearers who desire subtle cosmetic enlargement and color refinement (e.g., Hazel Brown, Sky Blue, Honey Grey) for professional and daily settings.
- High-Pigment Cosplay & Special Effects (SFX): Opaque coverage designs tailored for costume, entertainment, and fashion industries requiring high-contrast pixel distribution across dark irises.
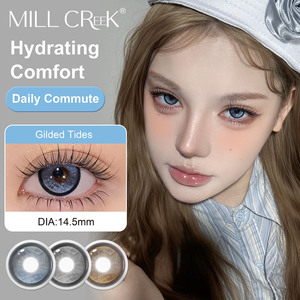
- K-Beauty & E-Girl Aesthetic Lines: Trend-driven, fast-turnaround optical collections inspired by East Asian cosmetic trends, focusing on limbal ring softness, pupil dotting transparency, and high hydration feeling.
- Prescription (Myopia) Cosmetic Lenses: Combining corrective optical power (ranging from -0.50D to -10.00D) with aesthetic tinting to convert regular vision care consumers into recurring cosmetic lens buyers.
Phase 2: Polymer Material Science & Ocular Health Engineering
The comfort and safety of a contact lens depend on polymer formulation and manufacturing precision. As a premier original equipment manufacturer (OEM) and original design manufacturer (ODM), our manufacturing facilities prioritize biocompatible monomer matrices:
PolyHEMA Hydrogel
Poly(2-hydroxyethyl methacrylate) offers time-tested mechanical stability, soft flexible fit, and 38%–42% water content ideal for daily and monthly cosmetic wear.
Silicone Hydrogel
Provides ultra-high oxygen transmissibility (Dk/t > 80), reducing corneal hypoxia risks during long wear cycles, making it suitable for premium brand lines.
Sandwich Color Technology
Color pigments are encapsulated between dual transparent hydrogel layers. Pigment never touches corneal or conjunctival tissue, preventing irritation.
Phase 3: Global Regulatory Roadmap & Certification Compliance
Compliance is the single biggest barrier to market entry. When choosing a colored contact lens supplier, brand founders must audit the factory's regulatory filings across target sales regions:
- United States (US FDA): Cosmetic and prescription soft contact lenses are classified as Class II medical devices. Sourcing factories must hold a registered FDA Establishment Identifier (FEI 3015587162) and submit medical device listing documentation.
- European Union (CE MDR 2017/745): European markets enforce strict MDR compliance under Class IIa classification. Products must be fully registered in the EUDAMED database with clear technical documentation.
- Quality System Management (ISO 13485:2016): Ensures every production batch—from raw monomer mixing to automated optical inspection and steam sterilization—is standard-compliant and fully traceable.
- Middle East & Latin America (SFDA / ANVISA): Requires factory Certificate of Free Sale (CFS), ISO certificates, and full chemical safety dossiers for localized market authorization.
Future Contact Lens Sourcing & Manufacturing Trends
Stay ahead of industry shifts with forward-looking supply chain strategies and technological innovations.
Daily Disposable Shift
Global consumer demand is rapidly shifting from annual lenses to 1-Day daily disposables, driven by eye hygiene awareness, travel convenience, and higher repeat purchase velocity for DTC brands.
Eco-Friendly Blister Packaging
Sustainable brands are adopting recyclable PP blister cups, reduced plastic weight foils, and FSC-certified paper secondary packaging to meet ESG criteria without compromising product sterility.
AR Virtual Try-On Integration
Modern B2B supply chains now integrate digital Pantone color mapping and 3D eye rendering, enabling brands to provide instant Virtual Try-On widgets on e-commerce storefronts prior to bulk ordering.
Our Enterprise Manufacturing Alliance
Direct-factory authority backed by four decades of continuous optical production, robust R&D, and worldwide brand distribution.
Two Owned Production Facilities
Our family manufacturing group was established in 1984 with Gansu Constar Technology Group and expanded through Hunan Liangguo Group (housing Hunan Haipuming Technology). As the international sales headquarters, Vibebeautylens Technology Co., Ltd. delivers direct factory pricing without intermediary brokers.
Global Brand Ecosystem & 15,000+ Designs
We proudly own and license recognized global optical brands including MILLCREEK, KSSEYE, Haipurecon, and DUOXIU. Our internal design bank features over 15,000 customized iris matrix patterns, supporting both ready-to-ship fast turnaround orders (7-10 days) and full OEM private label development.
Frequently Asked Questions (FAQ) for B2B Procurement
Answers to critical questions regarding minimum order quantities, compliance documentation, custom design, and logistics.
We are a direct factory owner. Vibebeautylens Technology Co., Ltd. serves as the international headquarters for our family-owned manufacturing group founded in 1984, which includes Gansu Constar Technology Group and Hunan Haipuming Technology (Liangguo Group). Clients work directly with the manufacturing source, guaranteeing raw material transparency, quality control, and factory-direct pricing.
Our facilities operate under certified ISO 13485 medical device quality management systems. Our products hold CE (MDR 2017/745) certificates for European markets and are manufactured in an FDA-registered facility (FEI 3015587162) supporting North American sales, alongside complete regulatory dossier support for SFDA and EUDAMED submissions.
For ready-to-ship stock designs from our 1,500+ standard SKU inventory, MOQs start as low as 50 to 100 pairs per design. For fully customized OEM color patterns, custom power ranges, or unique brand box packaging, MOQs generally start at 500 to 1,000 pairs per SKU depending on production line tooling requirements.
We utilize multi-layer Sandwich Printing Technology. Bio-compatible color pigments are embedded inside microscopic layers of hydrogel material (PolyHEMA or Silicone Hydrogel). This guarantees that color pigments never come into direct contact with the wearer's cornea, ensuring 100% color safety, zero dye leaching, and smooth hydration balance throughout 8+ hours of continuous wear.
In-stock wholesale orders are dispatched within 7 to 10 days globally. Custom private label OEM projects typically require 10–14 business days for artwork and sample verification, followed by 25–35 days for automated mass production, blister sealing, steam sterilization, and batch quality audit inspection.
Ready to Launch or Scale Your Private Label Contact Lens Brand?
Connect directly with our senior OEM/ODM optical engineering team. Receive custom design catalogs, material specification sheets, and factory-direct pricing within 24 hours.